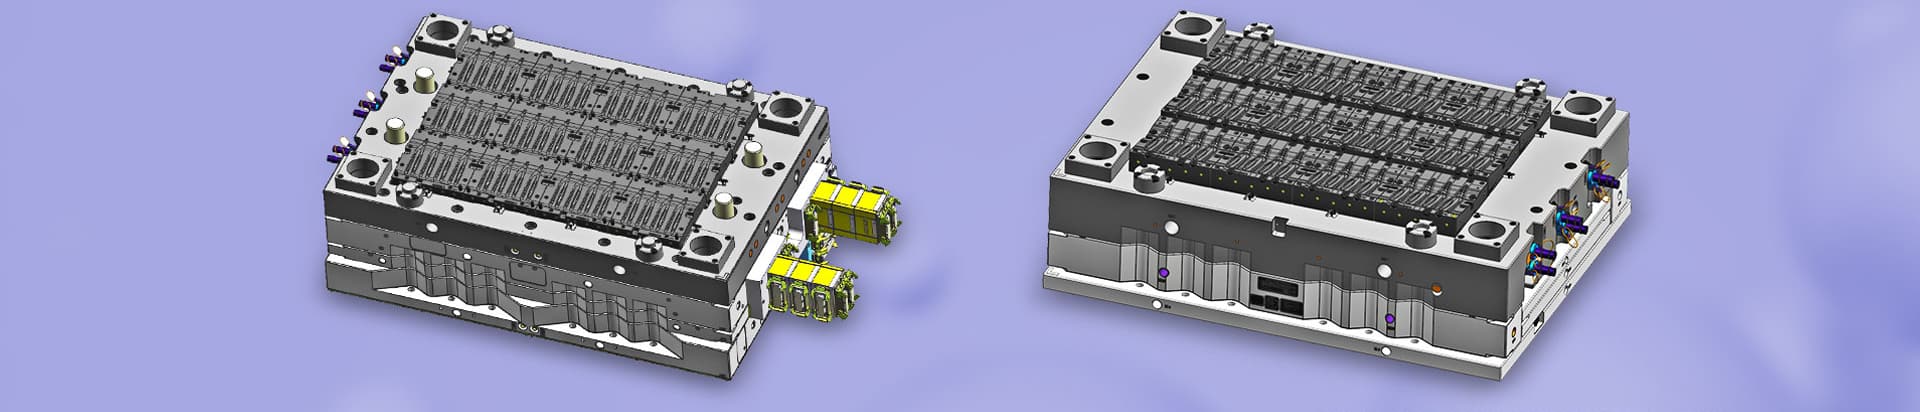
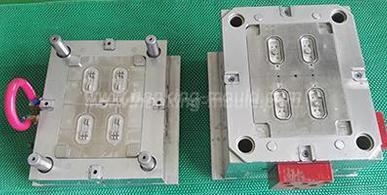
The key point is designed, good design comes to high yield production. Design level leads to lower costs and better efficiency.
80% of the troubles found during mould trial and mass production was due to worse design.
The yield can be increased dramatically when the below-mentioned principles are followed:
1. Part design stage: uniform thickness, non-uniform thickness will bring many troubles, e.g. air trap, warpage, ripple weld line, jetting, sink mark, void, short shot, and stress mark, etc. during plastic injection molding. Crystalline thickness shall be within nominal thickness ±10%, non-crystalline thickness shall be no over thickness ±25%.
Avoiding sharp corner at the turn, sharp corner is a place of stress concentration which would be a starting point of crack. High-stress concentration is found when worner radius is smaller than 25% of the part thickness. The corner can be strengthened when 75% of the part thickness is used for corner radii. The acceptable corner radius is 50% of the part thickness.
The draft angle should be large enough, the small draft angle will cause stress white at ejection and long cycle time. In principle, the draft angle should be 0.5-degree minimum and larger than 1 degree. The draft angle can be larger as long as customer accepted.
For plastic injection mould, shrinkage is also critical, most mould shrinkage is based on the wall thickness of 3.175mm, but the thickness of most current parts is less than 3mm, so the plastic mould cavity dimension is overestimated when use shrinkage based on 3.175mm which will produce a larger size part.
2. Mould design stage: sufficiently large gates and vents, flow balance and even cooling. Sufficient big gates and vents are the keys to successful injection molding. Small gates and vents would cause deffections include coronas, jetting marks, ripples, brown streaks, silver streaks, short shot, warpage, sink marks, weld lines, voids, burn marks, gas marks, etc.
In principle, the gate thickness should not be less than 60% of the part wall thickness where the gate is located. The depth of the vent depends on which plastic resin is used, vent quantity is more and deeper based on no flash.
Flow balance is the most importance principle of plastic injection mould, it means the melt fronts arrive the ends of the cavity at the same time no matter for a single cavity mould or a multi-cavity mould. A flow unbalanced mould is used, the most common defections include short shot, flash and warpage. When the gates number of an injection mould is the same for each cavity, a flow balanced mould needs a minimal injection pressure and clamp force. Good flow design support even distributions of melt-pressure, temperature and volumetric shrinkage, and stable and consistent mass production.
Another principle for plastic mould design is even cooling, the large difference of mould temperature between cavity and core sides will cause long cycle time and part warpage.
With CAE, adjust coolant temperatures and flow rates in order to have a symmetrical distribution of heat flux and residual stress to the center of the part wall which will minimize the bending moment applied to the part and stabilize the part dimensions.
3. Correct injection molding machine is also very important for getting good plastic part, before we start mould design, we should have a learn for customer's machine specification, it's not realistic to require customer use injection machine according to mould design, it is the best situation if customer can order new injection machine, if not a good designer should match his mould design with customer machine, and deny ripples, short shot, crack, warpage, flash, degradation, etc.
Injection parameter also helps much, the optimized injection time, ram speed profile, holding time and holding pressure vs time curve, etc.



 Call us on:
 Email Us:
 1st Floor, Block1, No.3 Beiting Road, Houting Community, ShaJing Street, Bao'An District, Shenzhen City, Guangdong Province, China
 English
 Deutsch
 italiano
 русский
 français
 română
 العربية
 Español
 Polska
 日本語
 한국어